Reduce trimming scrap and manual correction on variable 3D parts.
Combine part sensing and adaptive laser paths to trim eligible formed or molded components to the required contour despite normal geometry variation.
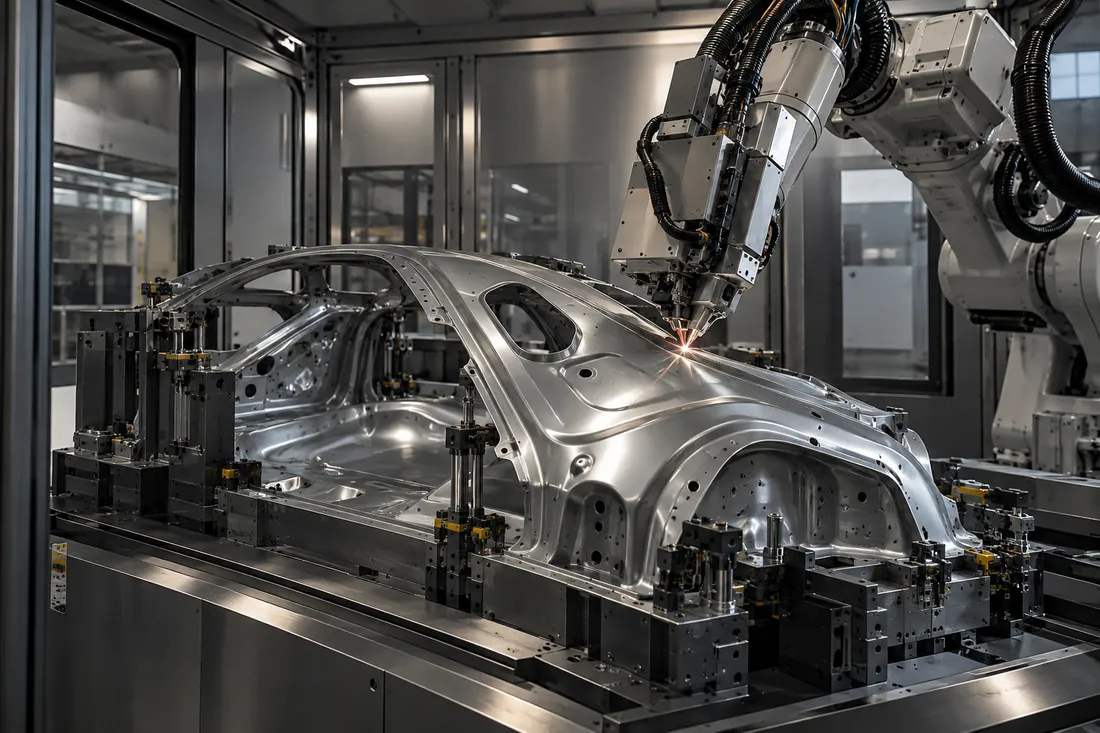
A fixed trimming path cannot follow a part that has moved or changed shape.
Forming and molding variation can put the real edge away from the nominal path. Operators then correct trims by hand, remake fixtures or scrap material after upstream work has already added value.
Scrap after value has been added
A poor trim can reject a part that already carries material and forming cost.
Manual edge correction
Rework adds touch time, reinspection and production delay.
Fixture burden across variants
Changing geometries drive additional setup and dedicated tooling.
Measure the real part and adapt the trim path to it.
RISEC scopes sensing, calibration, fixtures and a suitable robotic laser process around the part family. The cell identifies the relevant deviation, corrects the path and checks the finished edge.
Measure the actual geometry
Use suitable sensing to locate the contour and relevant variation.
Align and correct the path
Translate the measured position into an appropriate trim path.
Apply the laser process
Match source, optics, access and processing to the material.
Check the finished part
Include edge quality, dimensional verification and waste handling.
Where you recover value.
Reduce trim-related rejects
Follow the actual component rather than relying solely on nominal geometry.
Reduce manual correction
Move recurring edge work into the controlled cell sequence.
Improve flexibility between variants
Use sensing and recipes to reduce reliance on hard fixtures where the application allows.
$30,000/year
Eliminating 100 trim rejects per year on parts carrying $300 of material and upstream processing avoids $30,000 in example part losses.
How the process works.
Nominal geometry
Load the nominal geometry for the selected part family.
Measure part
Measure the actual formed or molded component.
Locate variation
Locate the deviation from the nominal contour.
Adapt path
Adjust the permitted trimming path.
Trim
Trim the required features inside the protected cell.
Inspect
Inspect the finished contour and edge quality.
How sensing supports work on non-nominal geometry
Published research on robot-based 3D measurement and laser scribing describes the role of sensing and coordinate calibration. It explains the alignment principle relevant to working on geometry that differs from the nominal model. Read the technical paper.
Equipment scope and common questions.
The scope includes material and thickness, measured variation, tolerances, fixture access, sensor calibration, source and optics, reach, enclosure, fume extraction and cut-quality trials.
Can it trim every composite or plastic?
Material response, emissions and edge quality determine the suitable laser process and sample qualification.
How much variation can sensing correct?
The measurement accuracy, part access and permitted path correction define the working range.
What is needed to assess a part?
Representative geometry or a sample, material specification, tolerance and the current trim and rework process.
Stop losing finished-part value at the trimming stage.
Tell us about the operation you want to improve. We will help define the equipment, integration and next steps for that application.